LOCATION
Alberta, Canada
CATEGORY
Shutdown & Maintenance | Sulphuric Acid Plant
INDUSTRY
Industrial Processing / Chemical Processing
Project Overview
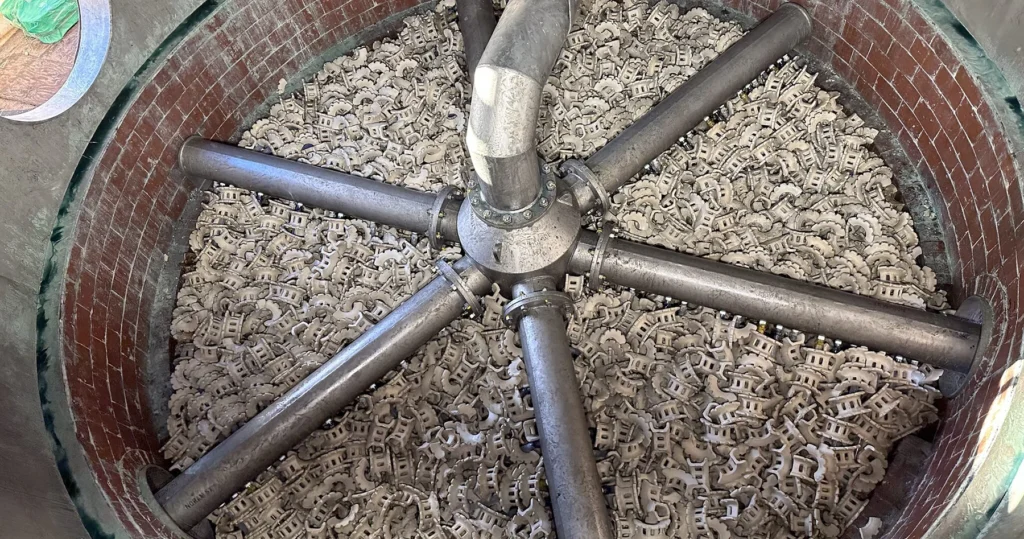
Our specialist maintenance team was engaged to complete a critical Sulphuric Acid Tower Distributor Piping Change-Out at a major industrial facility in Alberta, Canada.
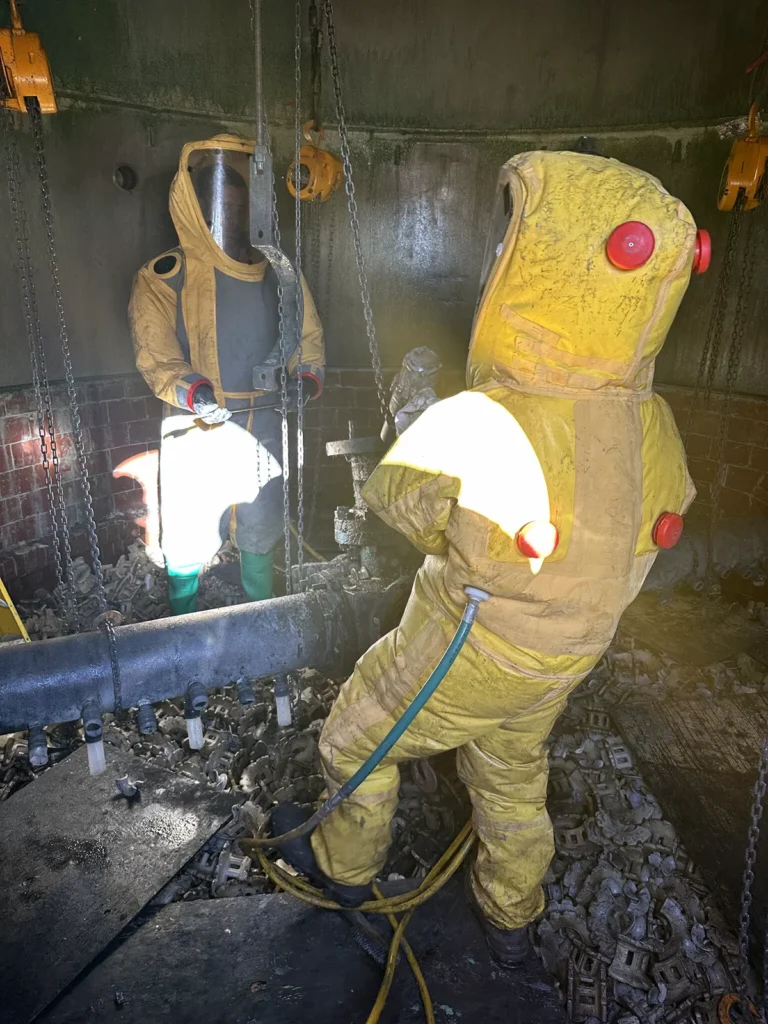
The project involved working within a highly hazardous, non-life-supporting environment to safely access, remove and replace existing distributor piping and associated components. Due to the challenging operating environment and restricted access, the works required specialist personnel, purpose-designed respiratory protection and fully encapsulated chemical-resistant suits.
Working to NoramSX™ specifications, our team successfully completed the piping change-out and reinstatement of ceramic packing, enabling the client to return the plant to operation with reduced shutdown downtime.
Scope of Work
The project scope included:
- Removal of approximately 950 mm of ceramic packing to provide access to the tower downcomers.
- Unbolting and removal of the existing distributor piping.
- Assembly and installation of the new distributor piping.
- Installation and connection of the new piping to the downcomers in accordance with MONDI™ specifications.
- Installation of new ceramic packing following completion of the piping works.
- Inspection and reinstatement of the work area.
- Completion of all activities within the scheduled plant shutdown window.
Specialist Working Environment
The nature of the work required our team to operate within a non-life-supporting environment, presenting significant challenges associated with hazardous atmospheres and sulphuric acid exposure.
To maintain the highest level of protection throughout the works, personnel operated in fully encapsulated chemical-resistant suits supported by dedicated breathing-air apparatus.
Our experienced team was able to combine specialist confined-space and hazardous-environment practices with the technical requirements of sulphuric acid plant maintenance, ensuring the work was completed safely and efficiently.
Project Resourcing
Key resources included:
- Experienced shutdown and maintenance personnel.
- Fully encapsulated chemical-resistant suits.
- Breathing-air apparatus.
- Specialist tools and equipment for piping removal and installation.
- Ceramic removal and reinstatement capability.
- Hazardous-environment safety and monitoring equipment.
- Project supervision and coordination.
Key Activities
The project incorporated a range of specialist activities, including:
- Fully encapsulated suit operations
- Breathing-air apparatus
- Sulphuric acid (H₂SO₄) works
- Shutdown maintenance
- Piping removal and installation
- Ceramic packing removal and reinstatement
- Downcomer access and connection
- Specialist hazardous-environment maintenance
Project Achievement
Delivering Specialist Shutdown Solutions
This project highlights our capability to undertake high-risk sulphuric acid maintenance and shutdown activities where specialist equipment, experienced personnel and disciplined execution are essential.
From hazardous-environment access through to piping replacement and ceramic reinstatement, our team provided an integrated solution that enabled the client to complete a critical maintenance activity efficiently and return the facility to operation ahead of schedule.